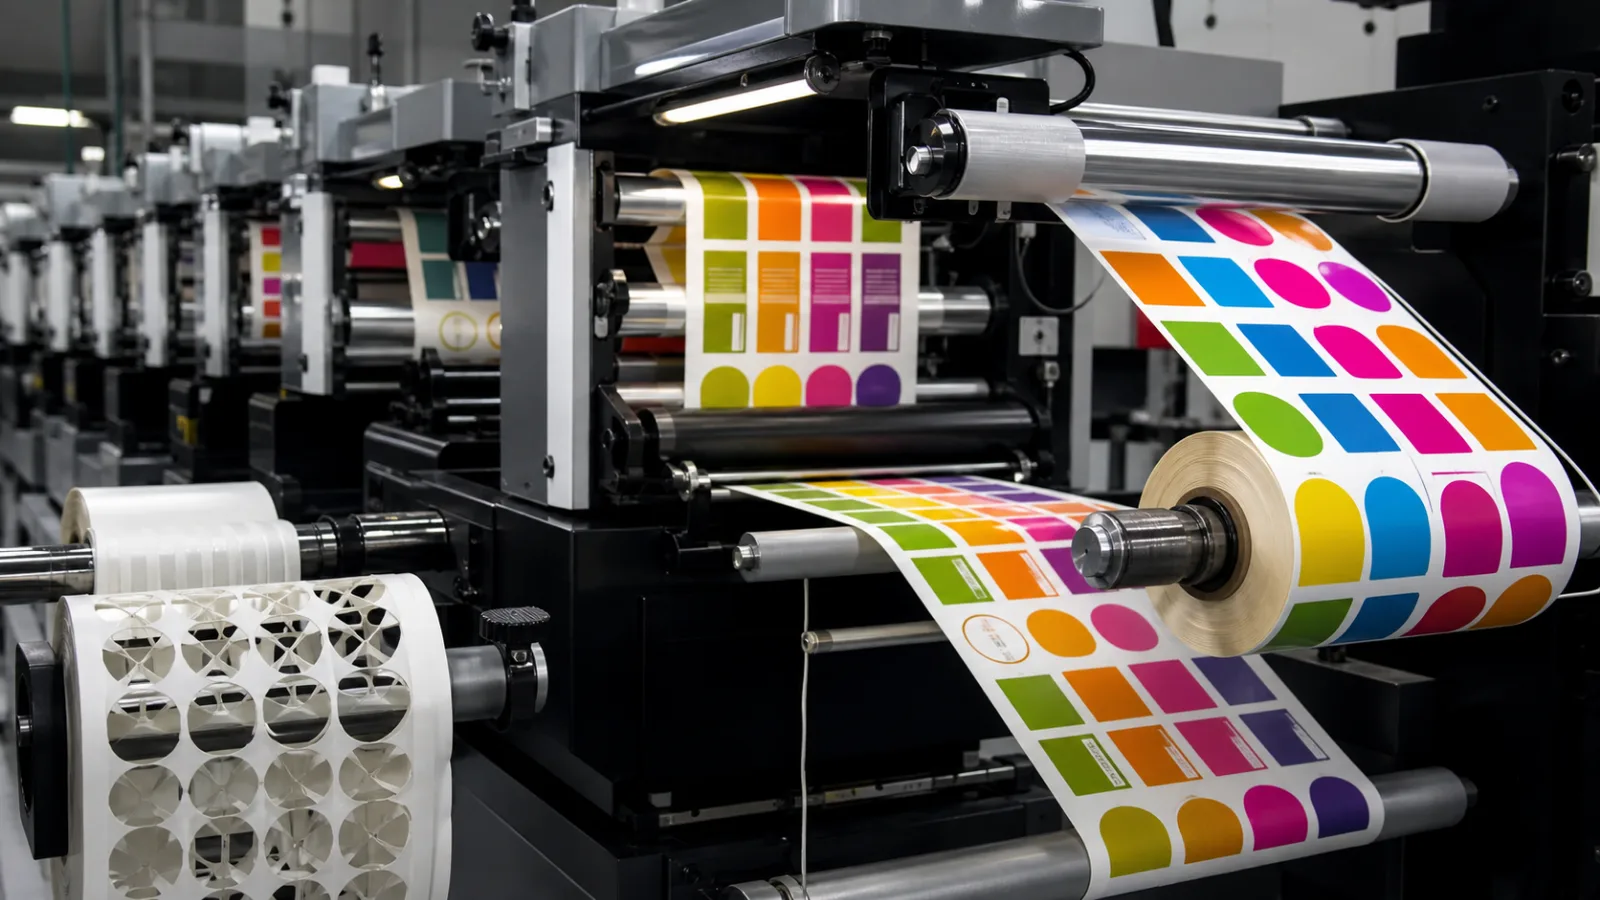
A pressure-sensitive label begins as a laminate: printable facestock, adhesive and release liner. It is normally printed in a narrow web, decorated and cut to shape before the unused surrounding matrix is removed and the labels are rewound.
Printing and decoration
Flexography is a productive route for established designs and uses plates to transfer fast-drying ink. Digital toner and inkjet presses remove the plate step and make shorter runs, frequent changes and variable information practical. Hybrid lines combine digital imaging with flexographic white, varnish, foil or other inline units.
Registration must hold across colours, coatings and the die-cut. Opaque white may be required on clear film. Varnish or laminate can protect an image from moisture, chemicals and abrasion.
A converted system
The die should cut the facestock without damaging the liner, while matrix stripping depends on label shape, gap, speed and material strength. Finished rolls must match the applicator’s unwind direction, core and outside diameter. Good label production therefore starts with the application: container surface, temperature, squeeze, exposure, dispensing speed and end-of-life route all influence the construction chosen for print.
Specify the construction from the container backwards
Facestock can be coated or uncoated paper, clear or opaque film, foil or a specialty material. The adhesive may be permanent, removable, repositionable, wash-off or engineered for cold, moisture, chemicals or a rough surface. The release liner carries the construction through coating, printing, cutting and dispensing.
A label that looks good on a flat test panel can fail on a small-radius bottle, a squeezable tube or a damp chilled container. Provide the converter with the container material, surface texture, curve, application temperature, service temperature and expected exposure. Test filled containers because flexing, condensation and product contact alter the result.
Printing routes
Flexographic presses use a plate and anilox roll for each colour, making them productive for repeat work and inline varnish or converting. Digital presses remove plates and suit short runs, multiple versions, variable codes and frequent artwork changes. Hybrid presses combine digital imaging with flexographic white, coating, foil or other conventional stations.
Substrate and design influence the route as much as quantity. A clear film may need an opaque white layer; metallic stock changes colour appearance; thermal facestock imposes heat limits. Review how flexographic printing works when evaluating a conventional quote.
Decoration and protection
Varnish or laminate protects ink from handling, moisture, chemicals and abrasion. It can also change gloss, flexibility and recyclability. Foil, embossing and tactile coatings add stations and registration demands. Leave quiet zones for variable overprinting and areas where a scanner must read a barcode.
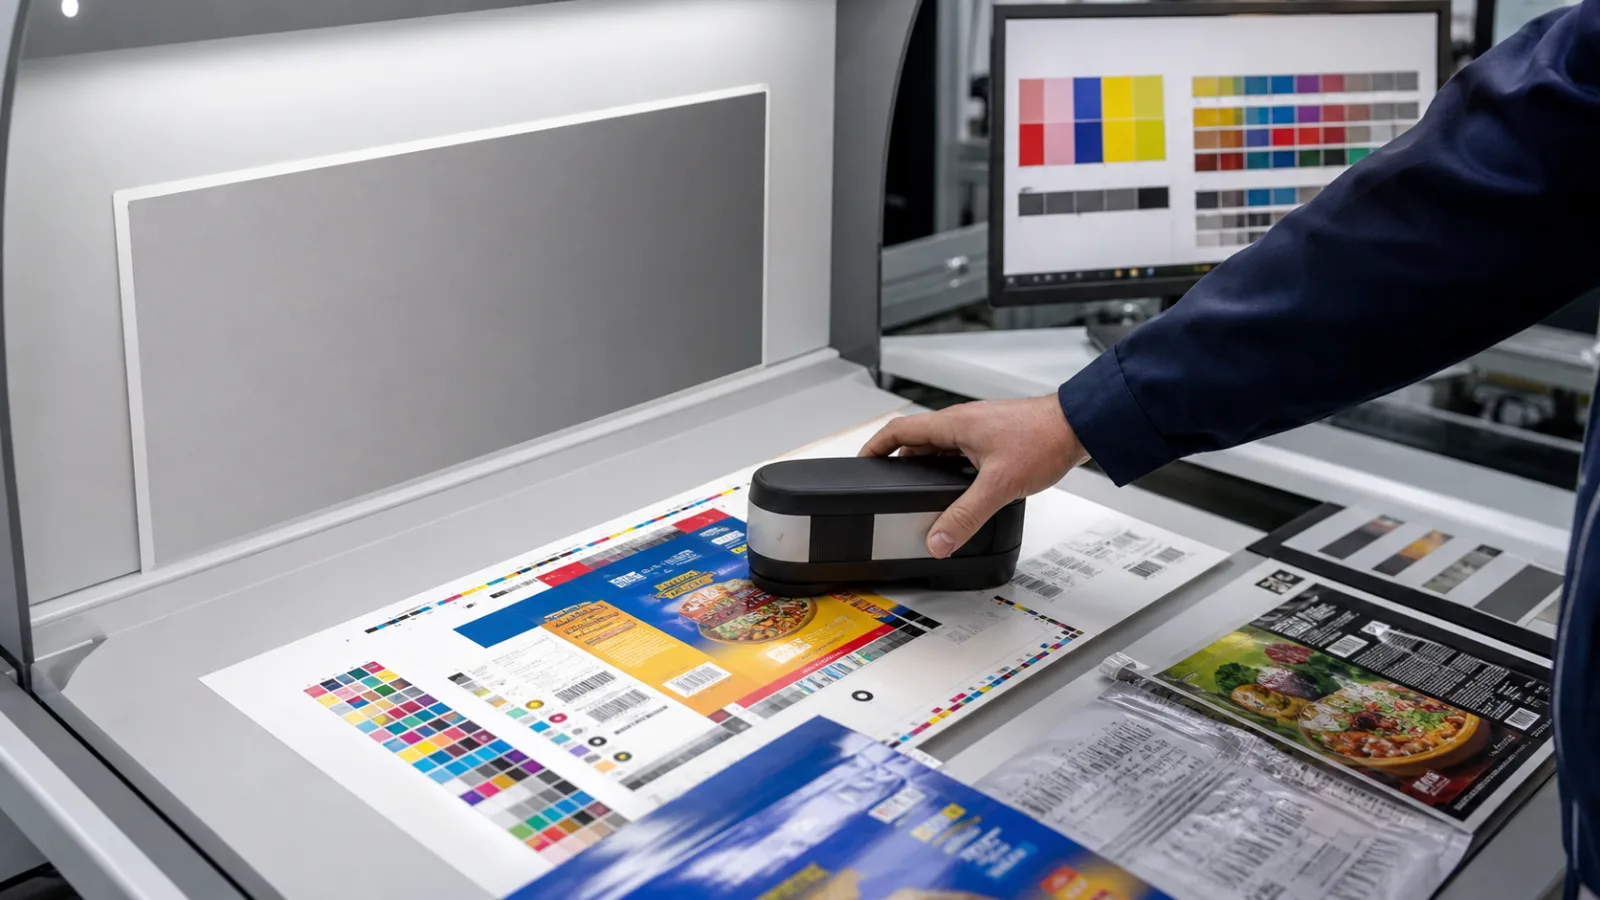
Colour approval should use the real facestock and backing. Clear labels viewed on a coloured container do not match an opaque white proof without deliberate simulation. The colour-management guide describes measurable approval conditions.
Die-cutting and matrix removal
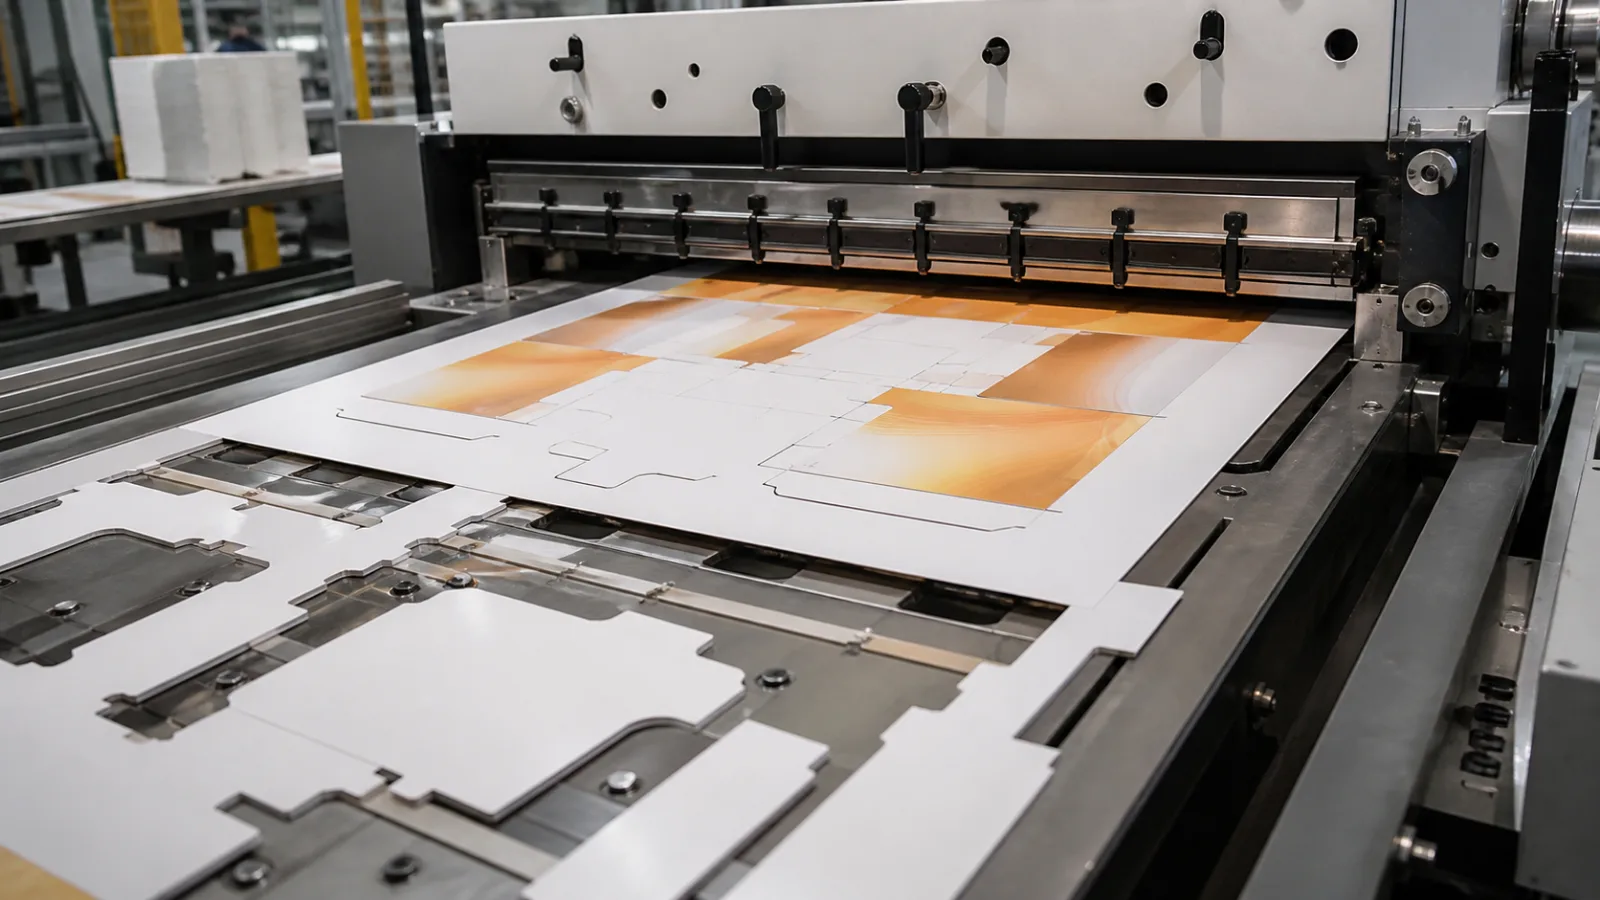
A rotary or semi-rotary tool cuts the label shape. The target is a clean facestock and adhesive cut without scoring the liner deeply enough to weaken dispensing. Small corner radii, narrow gaps and complicated shapes make the surrounding waste matrix fragile. Excessive speed or tension can snap that matrix and stop the line.
The converter adjusts die pressure, liner support, stripping angle and tension to the construction. Paper and film behave differently. The broader die-cutting guide explains cut tolerances and registration.
Roll finishing and application
After waste removal, the web is slit and rewound. Automatic applicators require a defined core diameter, maximum roll diameter, web width, winding tension and unwind direction. Label orientation on the roll must place the leading edge correctly. Splices need an agreed policy because some application lines cannot accept them.
Application trials should test dispensing speed, liner release, placement, wipe-down pressure and container handling. Adhesive needs time and suitable pressure to wet the surface; final bond can differ from initial tack.
Quality checks worth specifying
- Match facestock, adhesive and liner to the actual container and environment.
- Approve colour, opacity and finish on production material.
- Verify barcode grade and variable data after all coatings.
- Inspect register between print, varnish, foil and die line.
- Check liner damage, matrix breaks, adhesive ooze and edge lift.
- Confirm roll dimensions, orientation, splices and count.
- Run representative rolls on the production applicator.
For liner choices and recovery, see what release liner paper does. A pressure-sensitive label is a converted system: print quality matters, but application reliability comes from matching every layer and production step to the container’s real journey.
Common application failures
Edge lift often points to a mismatch between adhesive, surface energy, curvature or application pressure. Flagging at a seam can result from label stiffness and placement. Bubbles may come from trapped air, container contamination or an adhesive unsuited to the surface. Labels that dispense early or remain on the liner require checks of release, die damage, web tension and peel geometry.
Investigate with retained rolls and labelled containers. Record application temperature, dwell time and failure location. Changing facestock alone may hide rather than solve an adhesive or line-setting problem.
Questions to answer before quotation
- How many designs, languages and variable elements are included?
- Is the container rigid, squeezable, curved, textured or wet?
- Must the label survive refrigeration, chemicals, sunlight or abrasion?
- Does the line require a particular leading edge and unwind direction?
- Are opaque white, foil, laminate or tamper features necessary?
- How will facestock, adhesive and liner enter local recovery streams?
A complete brief lets the converter design the construction and process together, reducing late changes at press or application.
Roll quantity and winding
Do not calculate label count only from roll diameter. Facestock, adhesive and liner caliper, core size, winding tension and label pitch affect quantity. Ask for a stated count tolerance and method. If a filling line plans production from roll count, short rolls create avoidable changeovers.
Rewinding too tightly may cause adhesive ooze or liner distortion; too loosely can telescope in transport. Packaging, pallet orientation and storage temperature should protect rolls until application. Inspect edges and winding before loading the line.