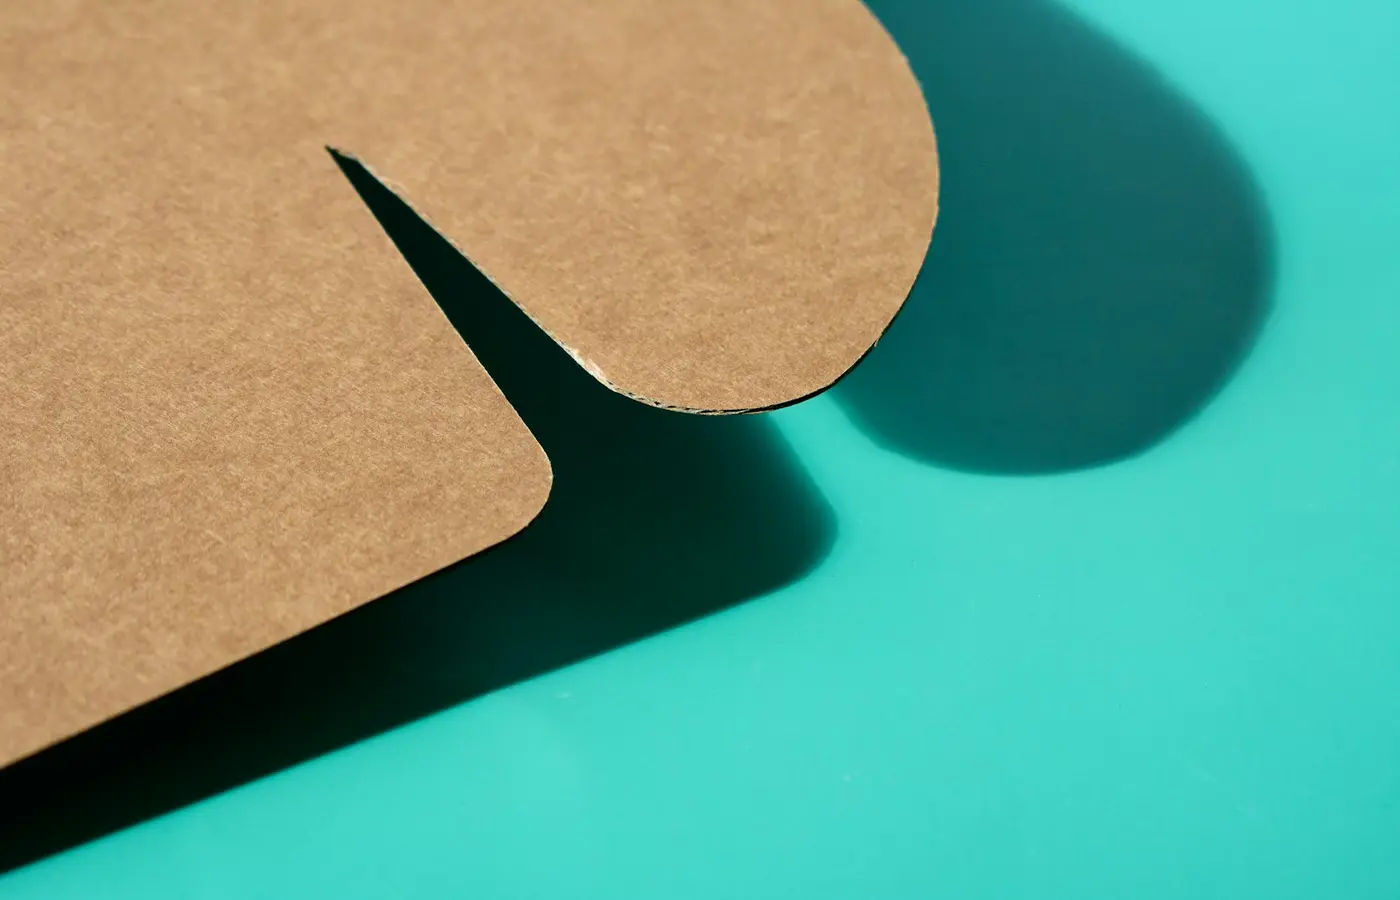
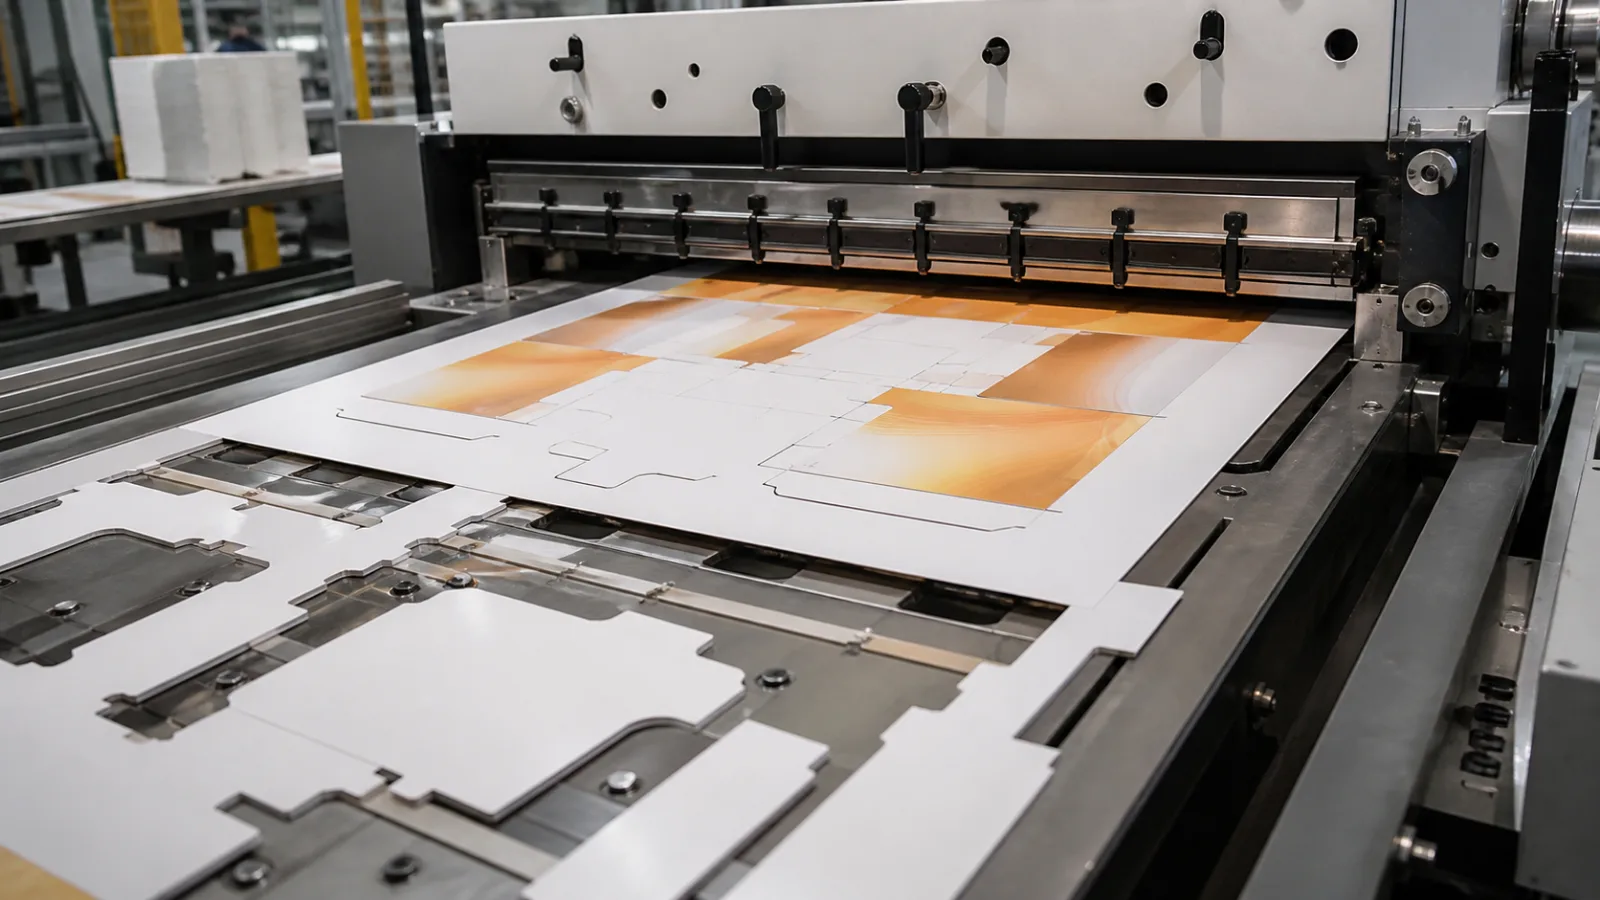
Die-cutting turns a printed sheet or web into a functional blank, label or component. Cutting edges define the perimeter, while crease rules and channels create controlled folding lines in paperboard. Perforation, stripping and embossing can be incorporated into the converting plan.
Accuracy starts upstream
The printed image, sheet position and cutting tool need shared reference points. Paper can change dimension with moisture and press conditions, and heavy ink or coating can affect the way a crease folds. Designers therefore keep critical graphics away from variable cut edges and provide clear bleed.
Rule height, bevel, rubber ejection and make-ready are adjusted for the material. A die that cleanly converts one board thickness may crush or incompletely cut another.
Judge the finished blank
Inspect cut edges, nicks, crease symmetry, cracking and panel dimensions. Erect the pack and run it on the intended filling or application equipment. Waste removal also matters: layouts that leave fragile matrix sections can limit speed. Effective die-cutting is not simply accurate geometry on a flat sheet; it creates a component that folds, feeds and performs consistently.
The dieline is production geometry
A structural designer supplies the cut, crease, perforation and sometimes glue or varnish boundaries as separate technical paths. The graphic designer places artwork around them, but should not redraw those paths or scale them independently. Work from the converter’s approved file and keep technical lines on named non-printing separations.
Bleed extends colour beyond the cut to absorb normal movement. A safe area keeps small type, barcodes and critical graphics away from cut or crease tolerances. The converter should state both values; there is no universal allowance for every press, board and die cutter.
Tools and pressure
In flatbed cutting, steel rules are formed into a wooden or composite base. Cutting rules penetrate the board, crease rules press it into matching channels, and rubber helps eject the sheet from the tool. Rotary systems use cylindrical tools and suit continuous or high-speed work. Digital cutting tables avoid a conventional die and are useful for proofs and some short production.
Rule height, bevel, hardness, ejection rubber and make-ready must match the substrate. Excess pressure can crush fibres, emboss unwanted marks or damage the reverse. Insufficient pressure leaves incomplete cuts. Tool wear changes the result through a run.
Creasing is not just a blunt cut
A crease displaces and restructures paperboard so it folds along a controlled hinge. Channel width and depth depend on board thickness, fibre construction, grain and coating. A poorly specified crease can crack the printed outer layer, produce an asymmetric fold or make a carton resist erection.
Grain should usually run parallel to the main fold lines where the sheet layout permits. Dense ink, film lamination and brittle coatings make testing more important. The folding carton guide links crease quality to packing-line performance.
Registration and dimensional movement
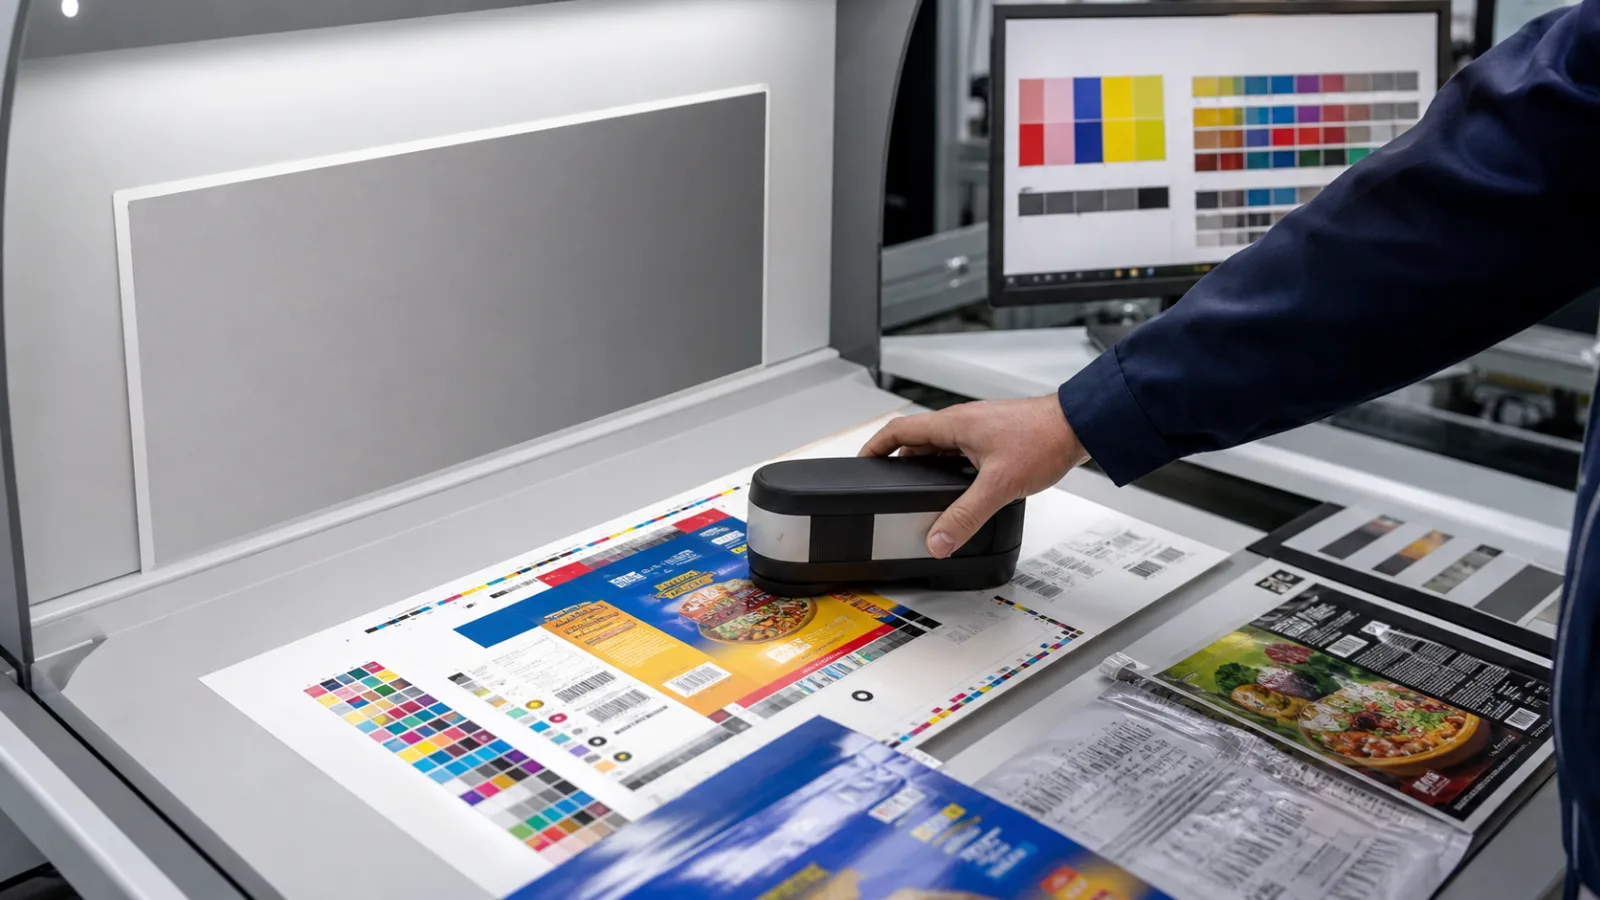
Printing and cutting use common registration marks, but paper is not dimensionally inert. Moisture, press drying, grain and heavy coating can alter sheet size or shape. The press operator, die cutter and designer need a shared tolerance plan. Critical borders that visually reveal tiny movement should be avoided near a cut.
For labels, the die cuts facestock and adhesive without seriously marking the release liner. For cartons, panel dimensions and creases must produce the intended three-dimensional structure. The correct inspection is application-specific.
Stripping and blank separation
After cutting, waste around the design is stripped away. Carton tools may separate individual blanks for the folder-gluer. Pressure-sensitive labels remove a continuous matrix from around labels. Small waste bridges, sharp corners and narrow gaps can break at speed, making an apparently efficient layout slow or unreliable.
Nicks deliberately retain blanks in a sheet until separation, but leave visible points if poorly positioned. Discuss them before approving exposed premium edges.
Artwork mistakes that reach the die cutter
- Technical dielines left as printable colours.
- Bleed missing around angled or curved cuts.
- Fine rules or type placed directly on variable cut edges.
- Varnish or laminate omitted from glue areas without testing.
- Barcodes crossing a fold, curve or seam.
- Front and back artwork built from inconsistent dieline versions.
- Structural changes made after proofs without a new folded proof.
Approve the converted object
Inspect cut cleanliness, dimensions, crease depth, cracking, delamination, nicks and surface marking. Fold or erect several proofs, not only the best one. Check glue joints, locks, windows and product fit. Then run production-equivalent blanks through the filler, cartoner or label applicator.
For paperboard selection, consult the paperboard grades guide. A board with different caliper or stiffness may require new crease channels and make-ready even when its GSM appears similar.
Handoff checklist
- Lock the converter’s dieline revision and scale.
- Separate cut, crease, perforation, glue and finish instructions.
- Apply supplied bleed and safe-area tolerances.
- Confirm grain direction, board caliper and coating.
- Produce a plain structural proof before final artwork.
- Approve printed, finished and converted proofs.
- Run a line trial when automated packing or application is critical.
Die-cutting is where a flat graphic becomes a mechanical component. Treating the dieline, material and finishing stack as production engineering prevents the most expensive failures from appearing only after the press run is complete.
Questions for the converter
- Which dieline revision and drawing scale control production?
- What cut, crease and print-to-cut tolerances should artwork allow?
- Which grain direction and board caliper were used to design channels?
- Will tooling be flatbed, rotary or digital, and who owns it?
- Where will nicks, ejector marks and stripping breaks appear?
- Does lamination, varnish or glue require a no-finish zone?
- Which measurements and erected-pack tests determine acceptance?
Put the answers on the job record. A verbal change to tooling or board can otherwise leave prepress, printing and packing teams working from different assumptions.