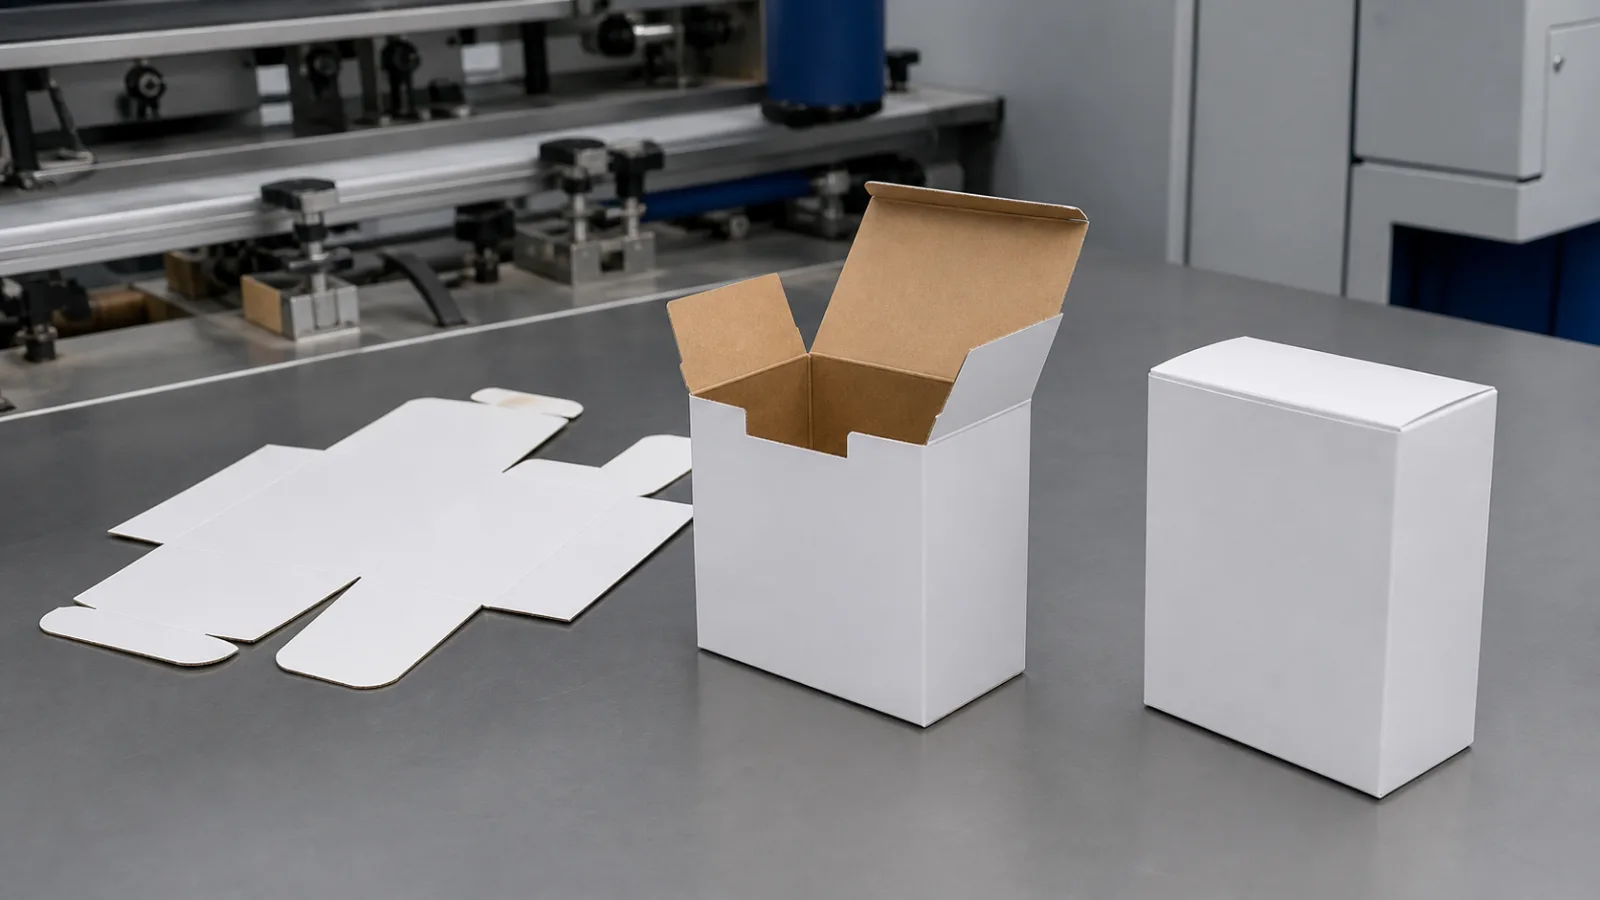
A folding carton is a paperboard pack delivered flat or pre-glued and erected for filling. Its panels, flaps, locks and glue areas are created from a printed board sheet by cutting and creasing. Cartons are widely used for food, healthcare, beauty, household and consumer products.
From board to blank
The converter prints the sheet, adds coatings or decoration and then uses a cutting forme to define the outline and crease channels. Creases locally reshape the board so panels fold predictably rather than crack. Grain direction, board thickness, coating and rule settings all affect that hinge.
Some designs are glued along one seam; others use crash-lock or hand-erected bases. Windows, tear strips and tamper evidence add converting steps and affect recovery choices.
Design around the product
Structural design must support filling equipment, distribution, shelf presentation and opening. The graphic file needs correct cut, crease, glue and no-print zones. Before launch, use production-equivalent board for line trials and transport testing. A lighter board may reduce material, but only if the complete pack still protects the product and runs reliably at packing speed.
Start with the product and packing line
Dimensions alone do not define a carton. A structural brief should state product mass, fragility, orientation, primary container, closure, tamper evidence, filling method, line speed, distribution environment and how the customer opens and disposes of the pack. A tuck-end carton packed by hand and a crash-lock carton erected automatically need different tolerances.
Use a plain prototype early. It should hold the real product, close without excessive force and expose access, rattle, compression or assembly problems before graphics make changes expensive.
Select board by performance
Solid bleached board, folding boxboard, solid unbleached board and recycled grades offer different combinations of surface, stiffness, bulk, purity and reverse-side appearance. Within each family, mills supply several grammages, calipers and coatings. The paperboard grades guide provides a structured comparison.
Stiffness is directional and strongly related to thickness. A bulky board may provide the required panel rigidity at lower grammage, but it must still print, score and run well. Food, healthcare and other controlled applications require documentation specific to the product, conversion and market.
Structural design and grain
Panels, dust flaps, tucks, glue seams and locks are connected by cut and crease lines. Grain direction should generally support the main folds and panel stiffness. Reversing it can change erection force and bulging. Curves, windows and tear features reduce material locally and need reinforcement or testing.
The dieline is controlled production geometry. Artwork should never independently redraw or rescale it. Keep critical content away from cut and fold tolerances, extend bleed correctly and protect glue areas from incompatible ink or coating.
Printing and surface finishing
Offset lithography is common for sheetfed carton work; flexography and digital printing serve other formats and run structures. Coated board supports fine graphics, while an uncoated or kraft surface creates a different tactile and colour result. White ink may be required over dark or transparent areas.
Varnish protects print and controls gloss. Lamination adds resistance and feel but can affect folds, glue and recovery. Foil, embossing and windows introduce their own registration and tooling. Approve the complete finish stack on the intended board rather than combining unrelated proofs.
Creasing and die-cutting
Crease rules press board into channels so fibres form a controlled hinge. Settings depend on caliper, fibre structure, grain, coating and lamination. Poor creases create cracking, bowed panels or high erection force. The cutting tool then defines the perimeter, slots and windows; stripping removes waste and blanking separates cartons.
Read die-cutting printed packaging for dieline, tool and tolerance details.
Folding and gluing
Folder-gluers pre-break creases, fold panels, apply adhesive and compress joints. Glue must bond to the exposed surface, so coatings and print may need to stop short of the seam. Verify joint strength after the specified cure and under expected temperature or moisture.
Cartons can be delivered flat, side-seam glued or with pre-glued automatic bases. The packer’s equipment determines orientation, tolerances and how consistent opening force must be.
Test the system, not the beauty proof
- Approve a plain structural prototype with the real product.
- Confirm board grade, caliper, grain and coatings.
- Review a printed proof for colour and technical separations.
- Inspect production die-cut and glued proofs.
- Run a representative quantity on the packing line.
- Test transport, stacking and climatic exposure appropriate to the route.
- Recheck opening, tamper features and disposal instructions with users.
Material reduction with control
Lightweighting can reduce fibre and transport mass, but only when protection and machine efficiency remain intact. A carton that collapses, jams or causes product damage shifts impact elsewhere. Remove unnecessary layers, optimise dimensions and compare board structures through testing. The sustainable packaging materials guide explains why recovery infrastructure and product protection belong in the same decision.
A folding carton is a printed mechanism. The successful specification connects board, grain, artwork, creasing, glue, packing equipment and distribution—not just the appearance of the front panel.
Common carton styles
Straight-tuck and reverse-tuck cartons use top and bottom flaps that close manually or by machine. Auto-lock or crash-lock bases arrive pre-glued and open into shape quickly, but require more board and controlled folding. Sleeves wrap around an inner tray or product. Gable and multi-panel forms create distinctive structures at the cost of more complex tooling and assembly.
Style names vary between suppliers. Use the approved dieline and erected reference as the contract, not a name alone.
Production tolerances belong in the design
Paperboard changes with moisture, and print, cutting, folding and gluing each add variation. A technically perfect zero-tolerance mock-up is not manufacturable. Ask for cut, crease, glue and register tolerances, then keep fine borders and critical copy clear of them.
Packing-line trials should include ordinary variation across the run rather than hand-selected cartons. Measure opening force, squareness and glue integrity after conditioning. That evidence is more useful than approving one flawless presentation piece.