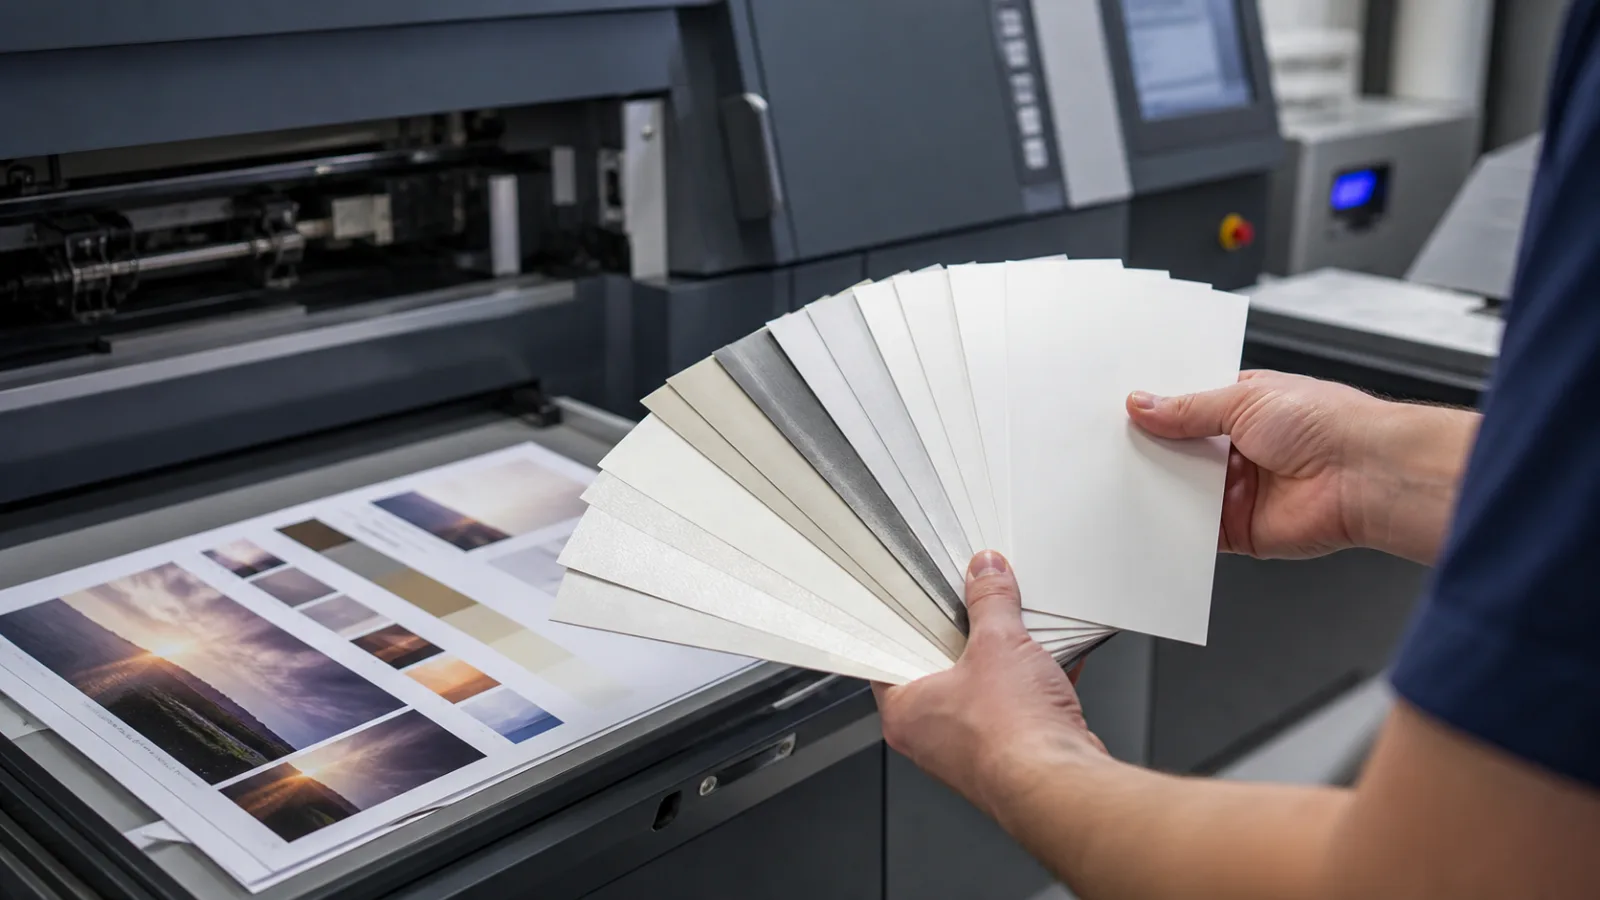
Packaging colour moves through displays, proofs, inks, substrates, coatings and different print processes. Colour management links those devices to defined targets so that decisions are based on measured conditions rather than on whichever screen happens to be nearby. When a campaign combines digital and offset printing, both routes still need a shared visual target.
Define the viewing condition
Agree on illuminant, measurement mode, backing and tolerances before comparing numbers. A transparent film, metallic substrate or textured board may need process-specific evaluation. Spot colours should include an acceptable visual and instrumental range, not only a name in a digital file.
Profiles describe how a press condition reproduces colour. They are useful only when the press, ink, screening and substrate remain within the condition that was characterised. Verification wedges and routine measurements show whether production is still there.
Build one approval chain
Calibrate monitors, use a contract proof suited to the process and preserve the approved physical standard. Communicate whether a conversion prioritises numerical closeness, clean separations or brand appearance on the actual pack. When a colour cannot be reproduced in gamut, approve the chosen compromise explicitly. That turns colour from a late press-side argument into a controlled production decision.
Define the print condition
A colour value has meaning only with context. Record printing process, ink set, substrate, white backing or opacity, surface finish, screening, measurement geometry, illuminant and tolerance. A brown kraft liner, clear film, metallic foil and bright coated board can produce visibly different results from the same digital values.
Process profiles describe a defined press condition. The press must be calibrated and kept within control before a profile can predict output. Profiling an unstable process merely records one unstable moment.
Separate calibration, characterisation and conversion
Calibration brings a device to a repeatable target. Characterisation measures how that state reproduces colour. An ICC profile describes the relationship for colour conversion. Verification checks that proof or press output remains close enough to the intended condition.
These steps are related but not interchangeable. Loading a profile cannot compensate for a dirty anilox, changing ink viscosity, worn plate, unqualified paper or drifting dryer.
Screens and proofs
Design displays should be calibrated and viewed in controlled light. A bright office monitor can make a printable image look dull by comparison. Soft proofing helps predict gamut limits, but it cannot reproduce metallic reflection, transparency, texture or gloss accurately.
A contract proof needs to simulate the relevant print condition and carry a measurable control strip. For transparent or metallic packaging, a physical drawdown or press proof on the real construction may be necessary. Document whether the proof represents colour only or also predicts trapping, opacity and finish.
Process colour and spot colour
CMYK builds colour from screened separations and is efficient for imagery. Dedicated spot inks can target brand colours, opaque whites, metallics and other effects beyond a process set. Expanded-gamut systems add fixed colours to extend range and reduce spot-ink changes, but require mature separation and process control.
A named spot-colour reference is a target, not a guarantee. Ink film thickness, substrate shade, varnish, lamination and backing alter appearance. Agree a measurable and visual tolerance on the production material.
Measure consistently
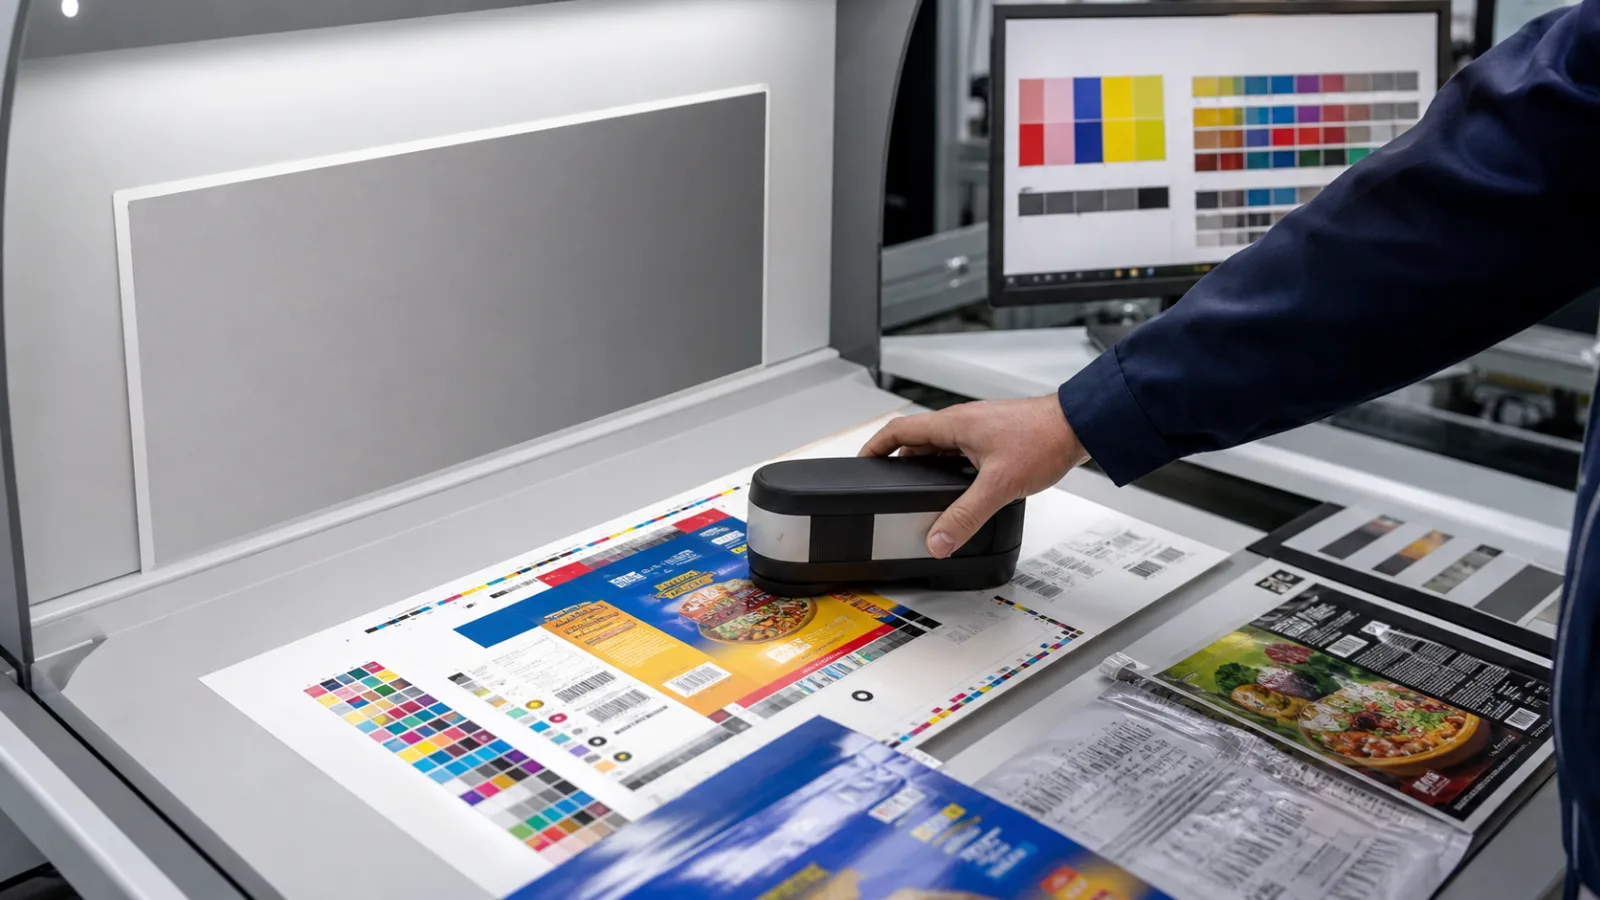
Spectrophotometer settings, aperture, backing and measurement mode must be standardised. proofs should be conditioned and measured in consistent locations. Density can help control ink film, while colorimetric values compare appearance; neither single number explains every defect.
Metamerism occurs when two proofs match under one light but diverge under another. Evaluate critical colours under the agreed standard viewing condition and, where the product requires it, under likely retail or daylight conditions.
The packaging workflow
- Establish master brand data and approved physical standards.
- Define each substrate and print process before separation.
- Calibrate displays, proofers and presses.
- Convert imagery and spot colours with documented priorities.
- Produce a contract proof and control strip.
- Set the press using ink, substrate and tooling in the target condition.
- Measure at normal production speed after the process stabilises.
- Retain signed proofs and measurement records for repeats.
For flexographic work, anilox volume, plate and impression affect ink film; review how flexographic printing works. In digital production, calibration and paper profiles serve the same need for a defined state; see how digital printing works.
Finishing changes colour
Gloss varnish or laminate can deepen apparent contrast. Matte film scatters light and may change dark colours. Reverse printing places ink behind a clear layer. Embossing changes the angles at which light reaches the surface. Measure and approve after the final finish whenever brand appearance is critical.
Adhesives and backing can also affect clear labels. Evaluate the label on the actual filled container, not only on a release liner. How label printing works connects colour to construction and application.
Common failures and controls
| Failure | Better control |
|---|---|
| Brand colour approved only on screen | Physical proof or drawdown on target substrate |
| Different suppliers use the same values but do not match | Shared target, measurement method and tolerances |
| Press reaches colour slowly with high waste | Fingerprint, stable standards and preset ink data |
| Proof matches before lamination but not after | Include final finish in approval |
| Spot colour is outside process gamut | Agree dedicated ink or documented closest process match |
| Measurements disagree between sites | Align instruments, backing, aperture, mode and proof condition |
Information for the print brief
List target colours, reference edition or spectral data, acceptable tolerances, viewing condition, substrate, backing, ink set, proof type, finish and approval authority. State how out-of-gamut colours should be handled. Keep one source of truth so a late PDF does not quietly replace approved targets.
Colour management cannot make unlike processes physically identical. It makes their limits visible, choices explicit and output measurable. That is what allows packaging produced on several materials or presses to feel like one controlled brand system.
Who should sign off colour?
Name one role with authority to approve the production target and deviations. Designers can judge intent, brand owners control identity, and printers understand process limits; an ambiguous group approval often creates contradictory instructions. Record the accepted sheet or roll, date, substrate, finish and measurement data.
For repeat orders, define when a new approval is required—for example after a material, ink, press or finish change. A retained reference can age or fade, so store it protected and review its validity rather than treating it as permanent truth.