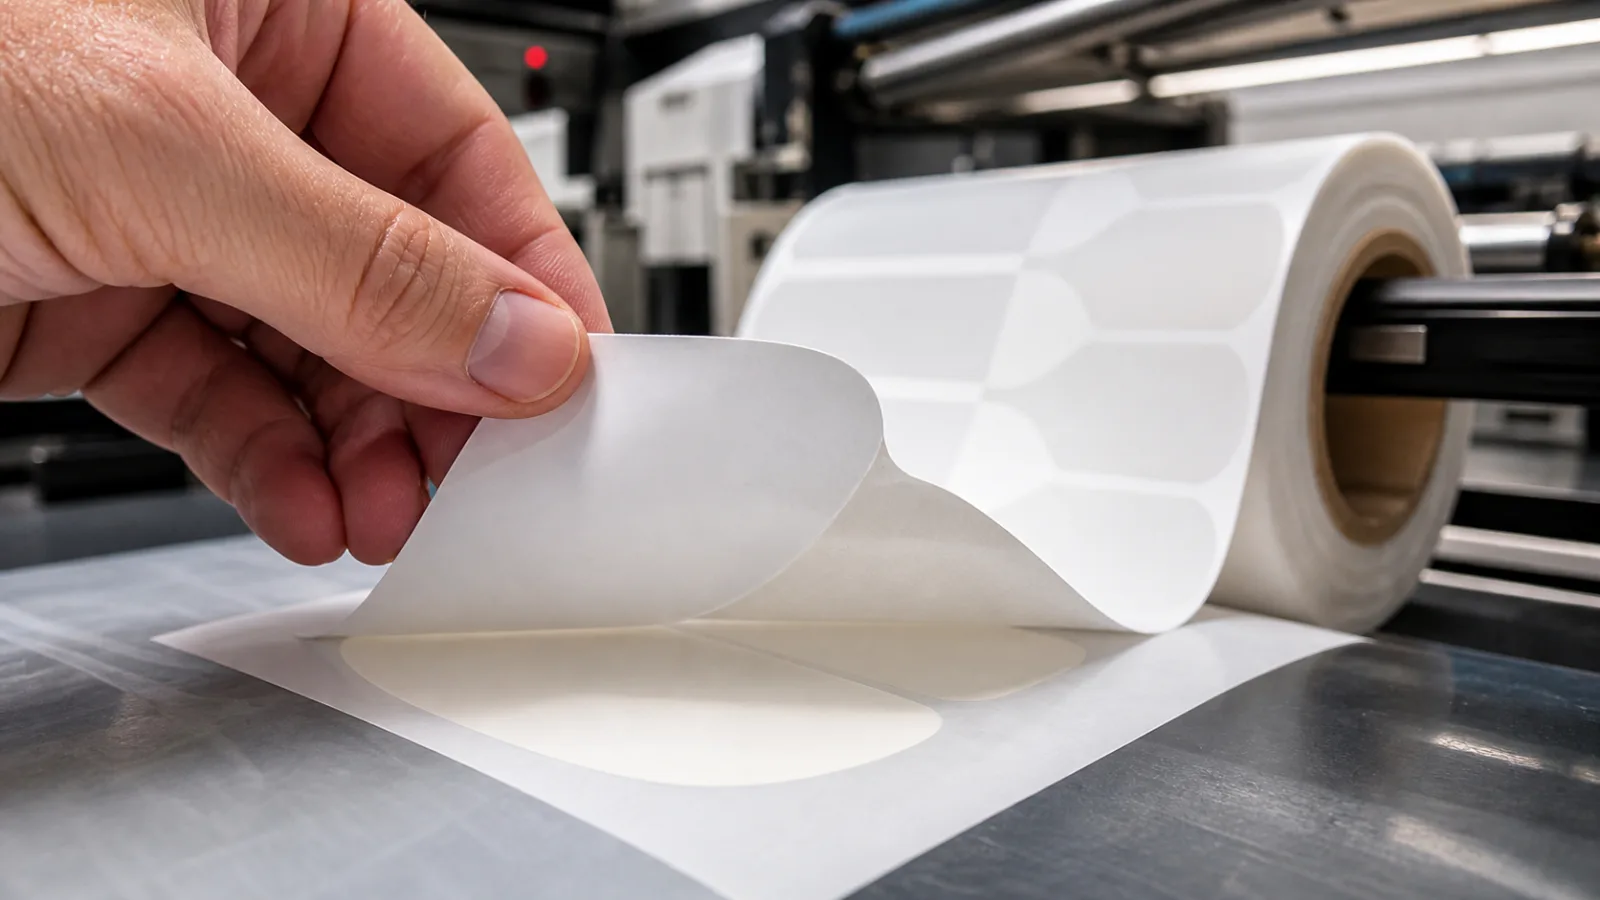
Release liner is the carrier that protects a pressure-sensitive adhesive until a label, tape or graphic is applied. A typical paper liner combines a dimensionally stable base sheet with a barrier or holdout treatment and a release coating, often silicone.
Why the liner matters
The coating must release consistently without transferring to the adhesive. The paper also has to run through coating, die-cutting, matrix removal, printing and dispensing under tension. Caliper variation, curl or weak internal bonds can disturb those operations even though the liner is not part of the final label.
Glassine and supercalendered kraft are common paper bases. Clay-coated kraft is used where stiffness, flatness or sheet converting is important. Film liners offer different strength and transparency profiles.
Look beyond release force
Specify die-cut resistance, tensile strength, moisture response, thickness and optical sensing alongside the release level. Recycling depends on collection and separation systems because the silicone-coated liner arrives as a concentrated production stream. Converters should discuss recovery options early, then protect that stream from contamination so it remains useful to a specialist recycler.
A liner is a process component
Although the customer normally discards it, the liner performs several jobs. It carries adhesive through coating and ageing, supports the facestock during printing, absorbs die-cutting pressure, allows waste matrix to be stripped, keeps rolls dimensionally stable and releases each label at the applicator peel plate. Reducing liner weight without checking those functions can increase breaks, missed labels and downtime.
Paper liner families
Glassine is dense, smooth and translucent. Its controlled caliper and surface suit roll-to-roll label converting. The glassine paper guide explains how refining and calendering create that structure.
Supercalendered kraft is also highly densified and smooth. Product terminology varies, so compare actual tensile, caliper and transparency rather than selecting from the family name.
Clay-coated kraft provides stiffness and flatness that can be useful for sheeted adhesive products and graphic films. Film liners offer high tear strength, consistent thin caliper and clear-on-clear processing, but introduce a different material and recovery route.
Holdout and release coating
The base needs sufficient holdout to keep the release formulation at the surface. Silicone is commonly cured into a controlled layer that provides predictable separation from the adhesive. Release is not simply “easy” or “hard”: it is measured under defined peel conditions and may change with speed, ageing and temperature.
Poor cure or contamination can transfer material, disturb adhesive performance or create unstable release. In a multi-liner construction, differential release may be deliberately engineered so one side separates before another.
Die-cutting and matrix stripping
The die should cut facestock and adhesive cleanly while leaving the liner strong enough to carry the labels. Deep cuts weaken it and can create dispensing breaks; shallow cuts leave label edges connected. The usable window depends on liner caliper consistency, die condition, facestock, adhesive and press pressure.
Matrix stripping adds tension. Sharp label corners, narrow waste lanes and small gaps increase break risk. A thinner liner may reduce material but also alter tool setup and web stability. The converter must test at production speed. See how label printing works for the complete converting sequence.
Automatic dispensing requirements
At the applicator, the liner bends around a peel edge while the label continues toward the container. Bending stiffness, release force, web tension and speed determine whether the label separates consistently. Optical sensors may depend on contrast through the liner. Splices, curl and thickness variation can interrupt a fast line.
Specify roll width, winding direction, core, outside diameter and splice policy with the label order. A liner cannot be evaluated separately from the applicator geometry.
Storage and moisture
Paper liners respond to humidity. Uneven moisture can produce curl, edge lift or dimensional change, particularly after one side has been coated. Keep rolls wrapped, supported and conditioned as directed by the supplier. Avoid heat that changes adhesive or release properties.
Recovery planning
Silicone-coated liner is clean and concentrated at factories, warehouses or application lines, which can make dedicated collection possible. It is not automatically accepted in mixed-paper bins. Availability depends on volume, contamination limits, transport distance and local specialist infrastructure.
Ask a recovery provider what grades it accepts, how rolls should be compacted or baled and which labels, cores or other contaminants must be removed. Document the route before claiming the construction is recyclable. Linerless formats can remove a carrier in suitable applications, but they introduce their own coating, printing, cutting and application constraints.
Questions for a liner specification
- Which base material, grammage and caliper are supplied?
- What release values and test conditions apply?
- Is the liner suitable for the die, press speed and label geometry?
- What tensile, tear and moisture tolerances are controlled?
- Will optical sensing and automatic dispensing work?
- Is a verified collection route available at the point of removal?
The right release liner is the one that protects adhesive and runs through every converting and application step with predictable release. Its value is measured in production stability, not in whether it remains visible on the finished product.
Lightweighting needs a line trial
Thinner liners can increase the number of labels on a roll and reduce roll changes, storage and transport. They also alter stiffness, tension, die-cutting tolerance and resistance to breaks. A calculation of material saved should include any rise in matrix failures, applicator stops or rejected rolls.
Trial the candidate through coating, printing, die-cutting, stripping, slitting and the fastest intended applicator. Include splices and the smallest label geometry. Retain release measurements before and after ageing.
Keep changes controlled
Because the liner is hidden from the end user, substitutions can appear harmless. Require notification when base paper, silicone system, caliper or manufacturing site changes. Link each finished label lot to its liner and adhesive lots so a dispensing failure can be traced. That discipline turns an invisible component into a manageable process variable.