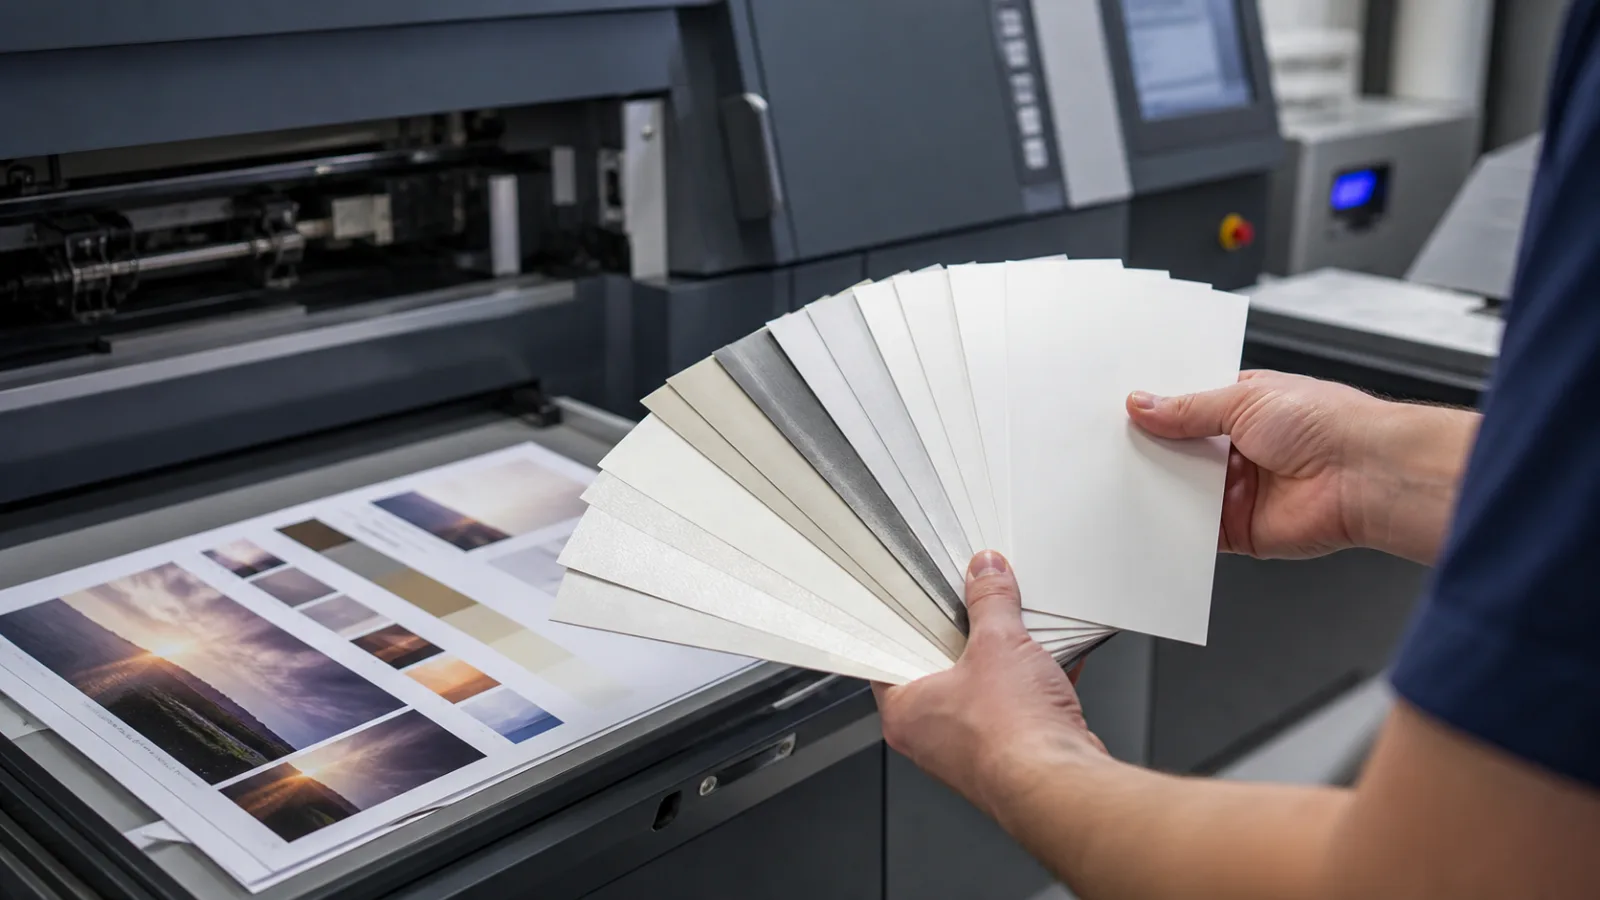
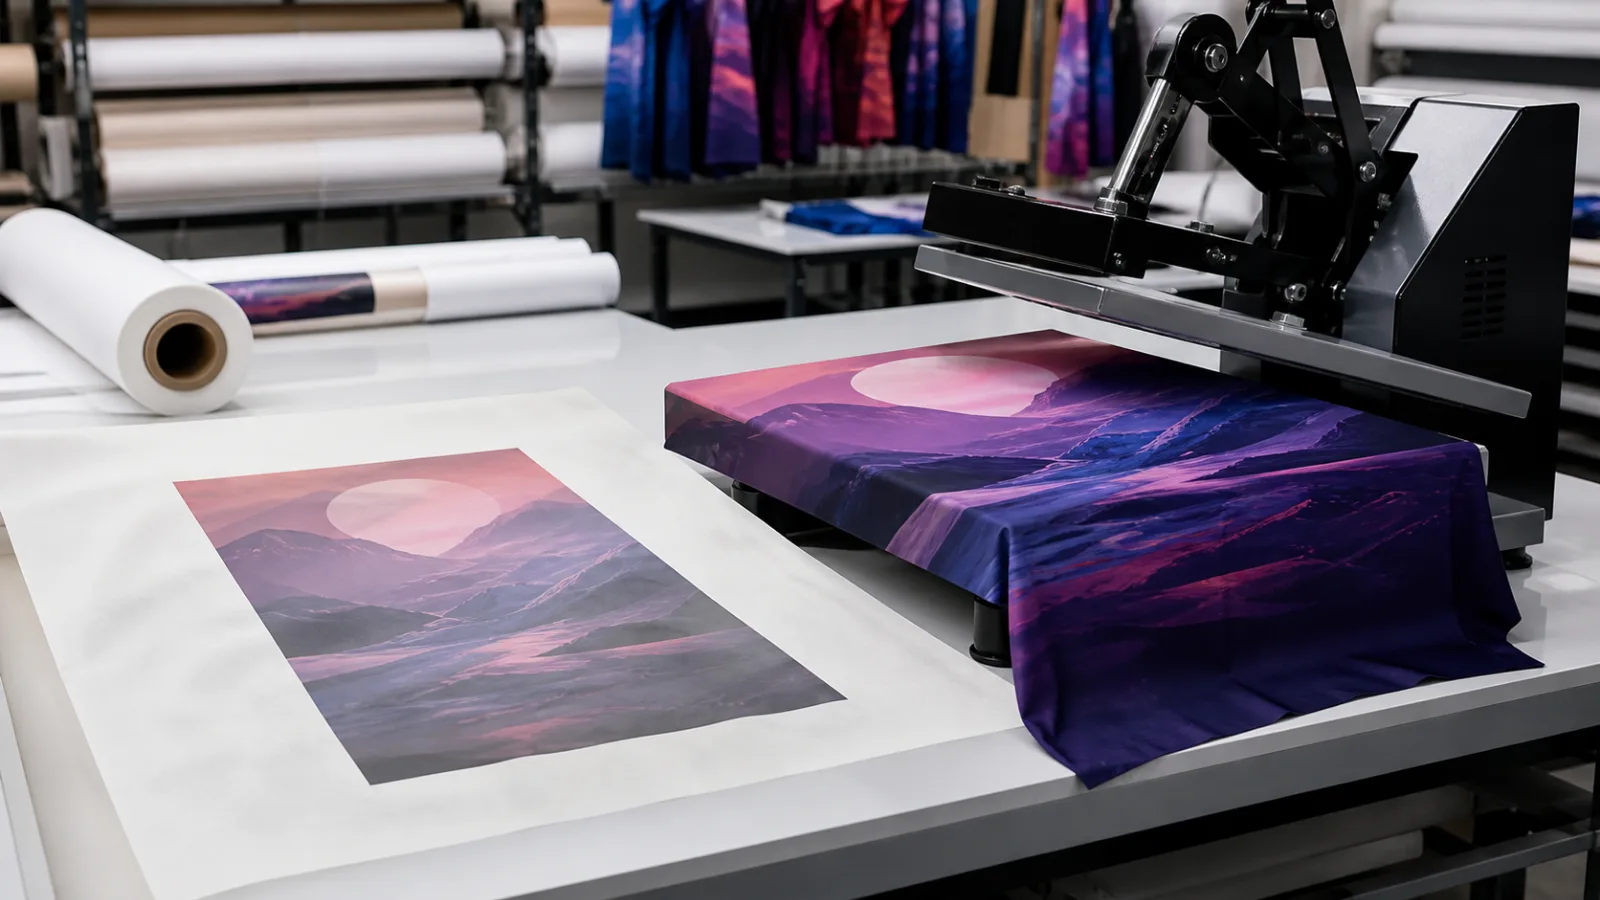
Sublimation paper is a temporary carrier used to transfer disperse dye to a polyester-rich surface. An inkjet printer first images the paper in reverse. Heat and pressure then cause the dye to enter a gaseous state and migrate into the receiving polymer.
The job of the coating
The paper must hold droplets with enough precision for a sharp image, dry at a useful production speed and release a high proportion of dye during transfer. If ink sinks too deeply into the fibre network, colour remains in the sheet. If the surface does not control liquid, lines spread and heavy areas can cockle.
Transfer settings depend on the ink, paper, textile or coated object, calendar or press and environmental conditions. More ink is not automatically better; excessive laydown can slow drying and cause ghosting or marking.
Selecting and storing paper
Match paper weight and release characteristics to ink coverage and equipment tension. Lightweight grades can support productive roll work, while heavier sheets may remain flatter under demanding coverage. Keep rolls wrapped until use and allow them to acclimatise in the production room. Moisture changes can affect feeding, drying and transfer consistency.
The image is intentionally temporary
In normal printing, the goal is to keep colour fixed on paper. Sublimation paper does the opposite: it controls liquid ink during printing, then releases dye efficiently under heat. The first print appears muted because its colour is judged after transfer. Artwork is normally mirrored so it reads correctly on the finished product.
The receiving material needs polyester or a suitable polymer coating because disperse dye forms a molecular bond within that polymer. Cotton does not accept the same permanent sublimation result without a separate treatment. Hard goods such as coated metal or ceramic require a compatible factory-applied or qualified coating.
What the paper coating controls
The receptive layer limits lateral droplet spread, supports sharp lines and keeps dye near the surface. It must dry quickly enough to avoid offsetting on a take-up roll, yet release under the time, temperature and pressure window used by the process. Paper formation and dimensional stability affect register in long web work.
Fast-dry and high-release are useful descriptions only when measured with the intended ink, coverage and equipment. A paper that releases strongly may behave poorly with a saturated design if drying or cockle is uncontrolled.
Paper weight and production format
Light transfer paper reduces roll mass and can heat quickly, which suits high-volume textile calendars when tension and ink load are controlled. Heavier paper may stay flatter on sheet heat presses and tolerate dense coverage, but it carries more thermal mass and cost. Choose by equipment and job rather than assuming heavier means higher quality.
Roll width, core, winding, edge quality and splice policy matter on continuous systems. Sheets need accurate squareness and reliable feed. For both, record the printable side and loading orientation.
A controlled workflow
- Build artwork in the colour workflow supplied for the printer, ink and target.
- Mirror the image and include sufficient bleed for placement variation.
- Load the correct coated side and select its print mode.
- Allow the print to dry without touching or winding too tightly.
- Secure paper and substrate so neither shifts during pressing.
- Apply the qualified time, temperature and pressure.
- Remove paper as specified and evaluate the cooled product.
Generic settings from another ink or blank are only a starting point. Excessive heat can scorch material or blur fine detail; insufficient energy leaves weak transfer. Uneven pressure creates patchy colour.
Common failures
| Symptom | Likely areas to investigate |
|---|---|
| Soft edges or bleeding | Excess ink, wrong paper side, unsuitable profile or high humidity |
| Cockled paper | Heavy coverage, moisture imbalance, drying or vacuum control |
| Ghosted double image | Paper or substrate moved during pressing or opening |
| Weak colour | Incomplete transfer, incompatible target coating or colour workflow |
| Speckles or marks | Dust, loose fibres, contaminated press surface or moisture |
| Transfer left in paper | Time/temperature/pressure mismatch or paper-ink incompatibility |
Change one variable at a time and keep labelled proofs. More temperature or ink is not a universal cure.
Colour approval belongs on the final material
The transfer print is not a contract colour reference. Polyester fabric shade, weave, coating, press condition and cooling all influence appearance. Approve colour on the actual production blank. If several products must match, profile and test each construction.
The digital prepress principles in how digital printing works still apply, but sublimation adds a second image-forming stage at the heat press.
Storage and handling
Keep unused rolls sealed and supported in a controlled room. Allow wrapped paper to acclimatise before opening. Handle print surfaces with clean dry hands, protect output from dust and avoid storing printed transfers for long periods unless the supplier qualifies that workflow. Humidity changes can alter drying, flatness and release.
Specify paper, ink, printer, target and press settings as one system. Sublimation paper is a temporary carrier, but its control over droplets and release directly determines sharpness, colour and production waste on the permanent product.
Textile-specific checks
Fabric construction changes the result. Knits may stretch during pressing, while woven material can reveal texture through fine graphics. Polyester content, optical brighteners, pre-treatment and base colour affect gamut and black density. Pre-shrink or condition fabric when the production method requires it, and maintain consistent tension through a calendar.
For cut-and-sew work, plan bleed for panel cutting and distortion. For finished garments, seams, zips and raised areas can prevent even pressure. Use fixtures approved for the product rather than forcing a flat setting.
Hard-substrate checks
Coated metal, ceramic and rigid blanks vary in coating quality and heat tolerance. Remove protective films, clean without contaminating the surface and use a fixture that applies even pressure. Approve each supplier and lot family; visually similar blanks can transfer differently.
In either route, judge wash, rub or exposure durability on the finished item. A vivid first transfer does not prove that the receiving coating will survive its intended service. The digital paper selection guide offers a parallel qualification method for paper-based digital work.